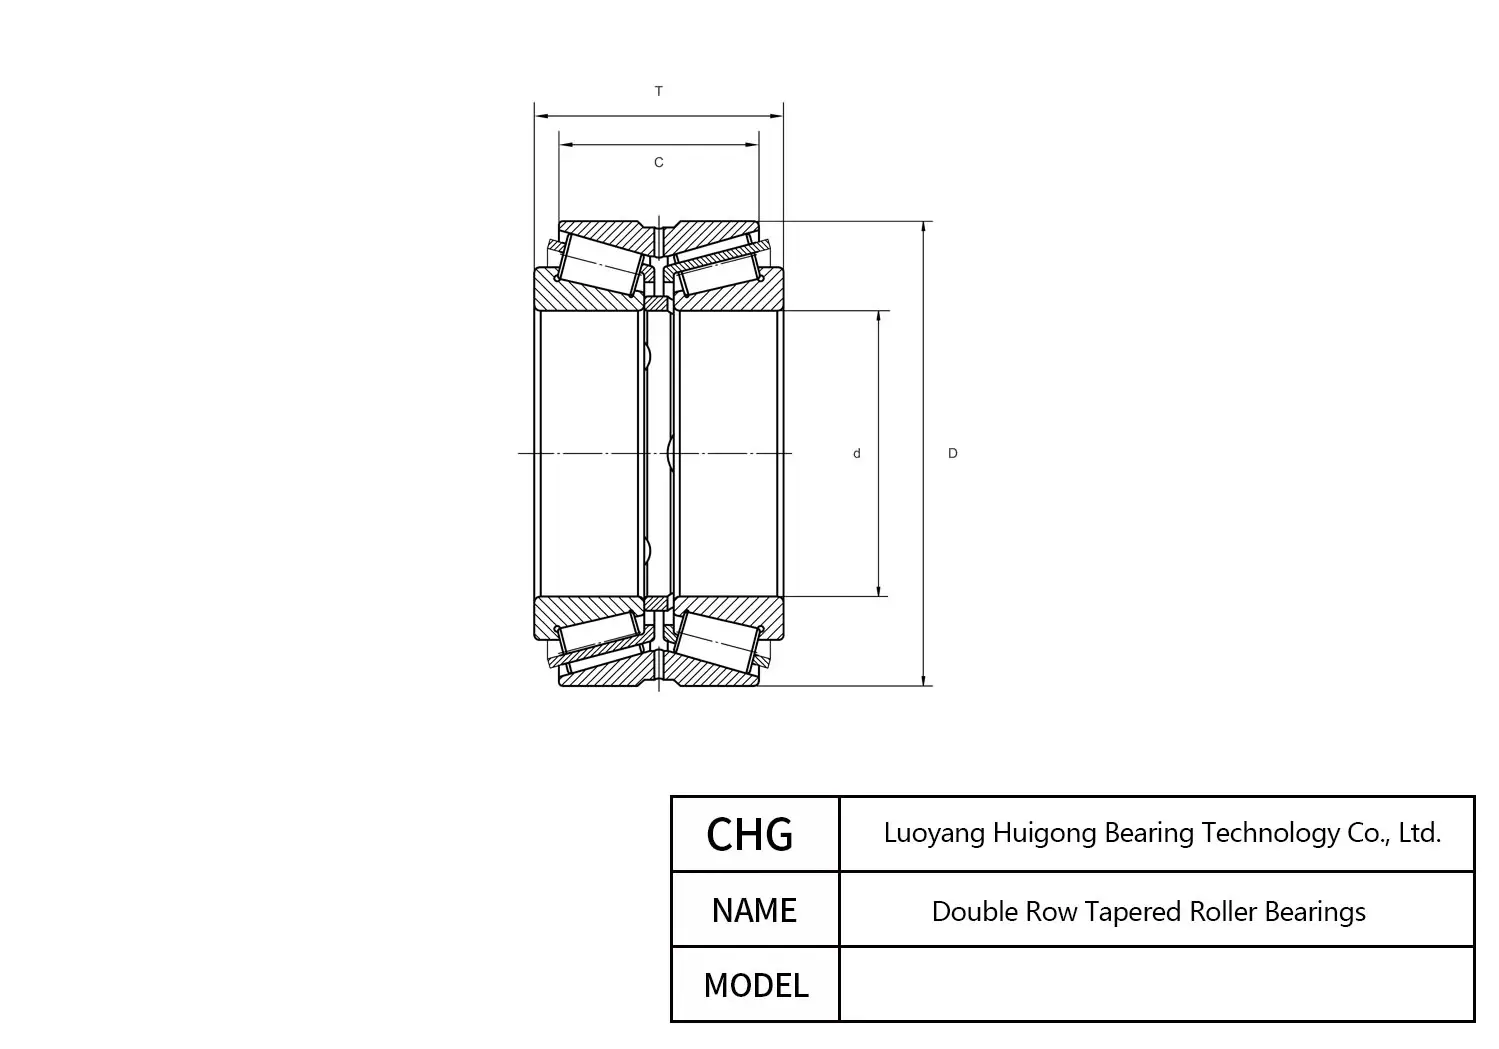
Manufactured by CHG Bearing, the HM959737DW is a precision Double Row Tapered Roller Bearings. Key dimensional parameters include a 305.08 mm bore diameter, a 500 mm outer diameter, and a 200 mm overall width. This component is designed to meet standard load requirements and ensure consistent operational performance. For comprehensive technical evaluation, please explore the detailed specifications, dimensional data, product images, and CAD drawings provided below. A complete PDF data sheet is also readily available for direct download to support your engineering and procurement needs.

HM959737DW - Double Row Tapered Roller Bearings
Technical Specifications
| Overview | |
|---|---|
| Part Number | HM959737DW |
| Brand | CHG® |
| Bearing | Double Row Tapered Roller Bearing |
| Characteristics | |
| Series | 370000 |
| Number of Rows | Double Row |
| Tolerance Class | Class 3 |
| Dimensions | |
| Bore Diameter (d) | 305.08 mm |
| Width (B) | 200 mm |
| Outer Diameter (D) | 500 mm |
| Bore Diameter Tolerance | 0 – +0.025 mm |
| Outside Diameter Tolerance | 0 – +0.025 mm |
| Inner Ring Chamfer | 6 min mm |
| Outer Ring Chamfer | 6 min mm |
| Inner Ring Assembly Width Tolerance | -0.065 – -0.01 mm |
| Outer Ring Assembly Width | 200 mm |
| Outer Ring Assembly Width Tolerance | -0.50 – +0.70 mm |
| Shaft Abutment Diameter | N/A mm |
| Housing Abutment Diameter | N/A mm |
| Lubrication Hole Diameter | 10 mm |
| Performance | |
| Basic Dynamic Load Rating C (kN) | 2380 kN |
| Basic Static Load Rating C0 (kN) | 4740 kN |
| Material | |
| Mass (kg) | 146 kg |
| Ring Material | Case-Hardened Steel / Bearing Steel |
| Cage Material | 08Al Steel / Grade 10 Steel |
| Lubrication Groove Width | 40 mm |
| Roller Material | Bearing Steel |
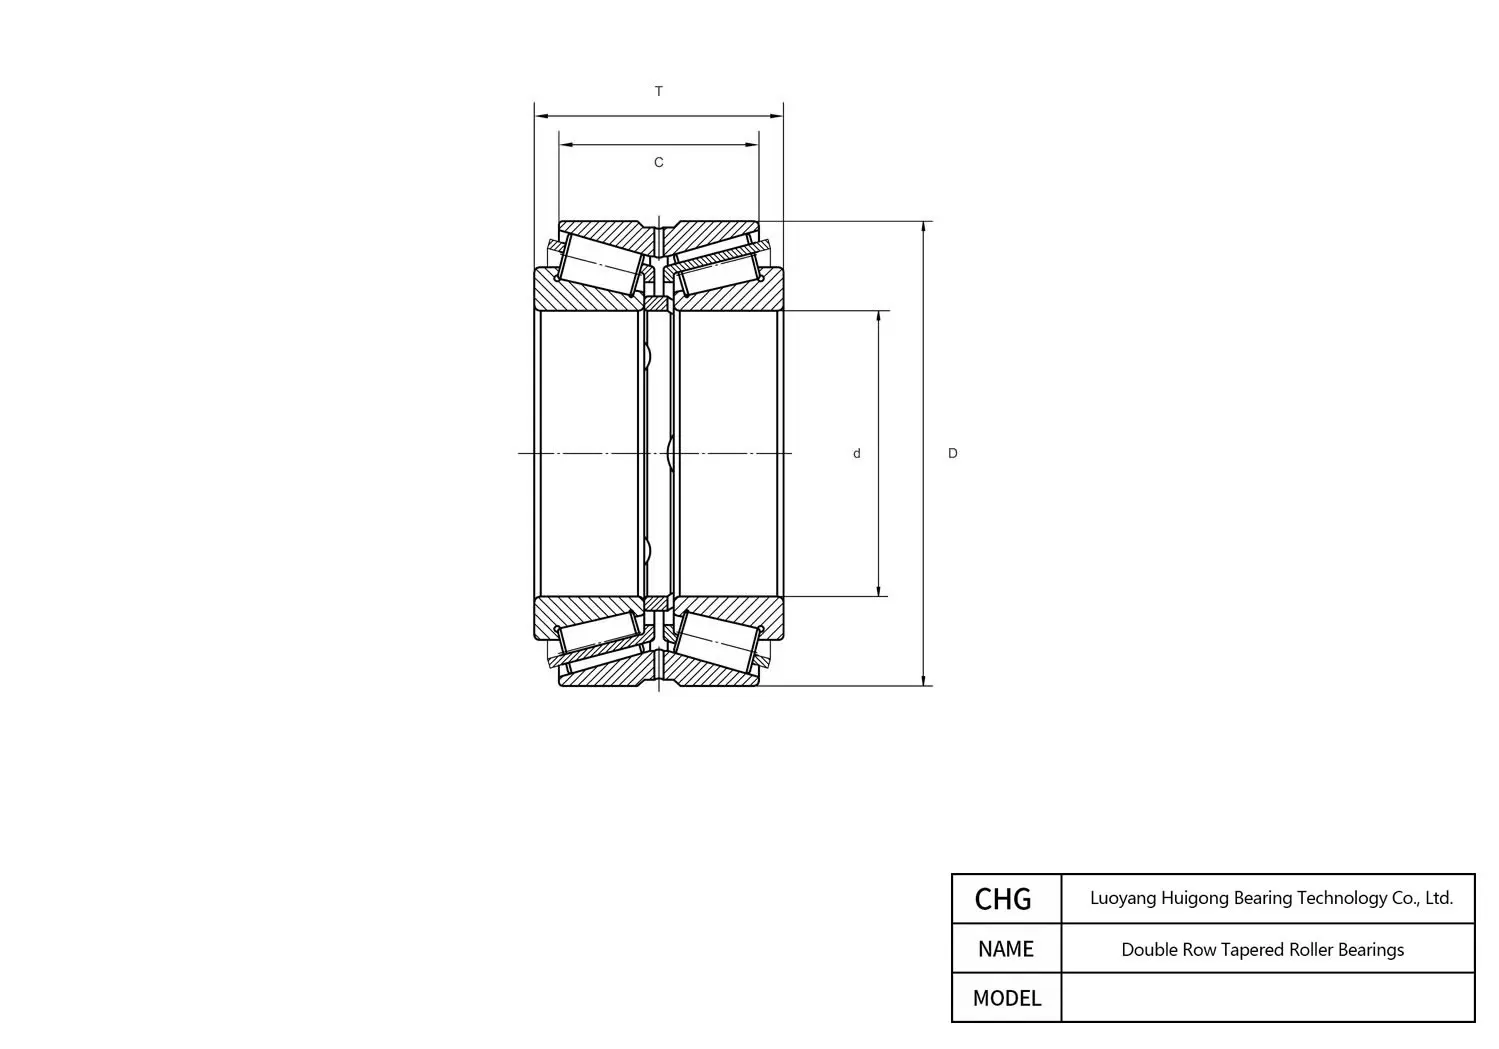 HM959737DW 500 mm 305.08 mm
Frequently Asked Questions about HM959737DW Double Row Tapered Roller Bearings
Find key technical answers regarding dimensions, specifications, and replacement options for this model.
As standard production, CHG Bearing subjects HM959737DW to precision bainite or martensite quenching, offering dimensional stability up to 120°C (248°F). For high-heat processing equipment, CHG Bearing also supplies custom S0 (150°C), S1 (200°C), or S2 (250°C) stabilization heat treatments upon request to prevent residual austenite transformation.
In its sealed configuration (Open Type), CHG Bearing pre-charges HM959737DW with premium wide-temperature lithium-complex or polyurea grease, calibrated to a 30%–35% cavity volume ratio. For open-type variants, synthetic PAO or refined mineral lubricating oils with appropriate EP (Extreme Pressure) additives should be circulated.
To extend the trouble-free lifespan of CHG Bearing HM959737DW, preventive maintenance routines should monitor operating housing temperature (normally maintaining below 70°C) and conduct regular vibration FFT analysis to identify early raceway micro-pitting before unexpected line halts occur.
Each HM959737DW produced in CHG Bearing manufacturing facilities features accurately profiled corner chamfers complying with DIN 5412 / ISO standard corner radii. When designing mating shafts and housing shoulders, machining an undercut or fillet radius strictly within the inner ring clearance limit (305.08 mm bore side) ensures perfect planar contact without edge binding.